Smart factories are raising the bar for machine design
As factories adopt more automated, intelligent machines, manufacturers expect equipment that supports higher availability and protects uptime. Machine builders can meet those expectations by treating switching, motor starting, control power, and safety as deliberate design decisions rather than commodity component selections.
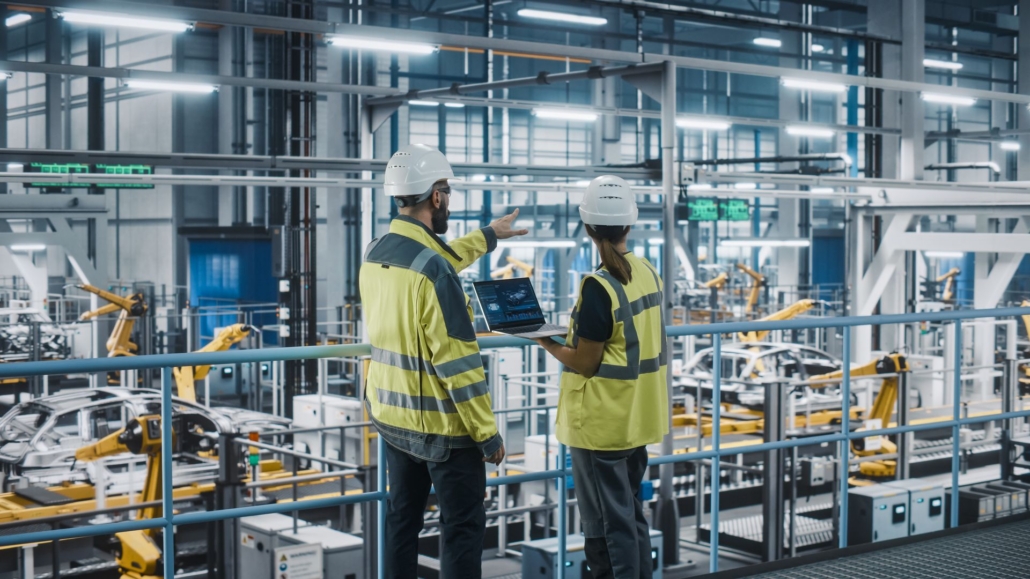
Smart manufacturing is transforming the factory floor and changing what manufacturers expect from their equipment. Performance and reliability still matter, but machines must now integrate easily with the rest of the line, report on their own condition, and remain available as one link in a tightly synchronized process. When a machine malfunction takes down an entire production line, the machine builder’s reputation is on the line.
Factory uptime often depends on upstream electrical choices that end users rarely see. By moving past commodity component selection and designing for real-world factory conditions, machine OEMs can reduce avoidable interruptions. The following design considerations can help them engineer greater reliability into their equipment.
Design switching for unstable supply conditions
Supply-voltage disturbances can originate outside the factory or within it, such as when large motors start. Even brief voltage dips can cause conventional AC contactor coils to chatter or drop out, interrupting motor operation and increasing contact wear. In some cases, these disturbances can lead to welded contacts—turning a momentary electrical event into a longer service interruption.
AF contactors address this vulnerability with an electronically controlled, wide-range coil. By regulating the voltage applied to the coil, AF technology supports stable switching despite supply-voltage fluctuations and can ride through short voltage dips within its specified operating limits.
Short-circuit coordination addresses another threat to availability. A tested starter and protective-device combination with Type 2 coordination helps ensure the starter remains suitable for operation after a short circuit. With Type 1 coordination, repairs or replacement may be needed before operation can resume.
Match motor starting to the load
Across-the-line starting applies full voltage to the motor immediately, creating electrical and mechanical stresses that can increase wear on driven equipment, such as conveyor systems. Variable-frequency drives can reduce starting stresses, but their speed-control capabilities may be unnecessary for a full-speed application.
Softstarters provide a middle ground: controlled starting and stopping without continuous speed regulation. By gradually increasing the voltage supplied to the motor during startup, they reduce starting current and help the load accelerate smoothly. Softstarters can also ease the transition to a stop where the application requires it.
Built-in bypass contactors address another design consideration: heat inside the control panel. Once the motor reaches full speed, the bypass carries current around the softstarter’s power semiconductors, reducing power losses and heat generation during normal operation.
Stabilize the control core
Momentary supply interruptions or sudden current demands from DC actuators and solenoids can pull down the 24 V DC supply, potentially resetting controllers and connected devices without logging a fault code. These “ghost stops” can be difficult to diagnose if the interruption leaves little useful fault information.
Industrial power supplies with built-in power reserve can accommodate short-duration load demands without requiring the supply to be oversized for those peaks. ABB’s CP-S.1 range, for example, provides 150% of rated power for five seconds to support heavy-load starting.
Capacitor-based buffer modules help keep controls powered during brief supply interruptions. They store energy and maintain the 24 V DC supply when incoming power is lost, without batteries or routine battery maintenance. The available backup time depends on the module and the load it supports.
Unexpected equipment failures can lead to costly downtime and damaged assets. Measuring and monitoring relays provide continuous supervision of critical electrical and process parameters, helping identify abnormal conditions before they become failures. They can detect phase loss, phase imbalance, incorrect phase sequence, and overvoltage or undervoltage, as well as overloads, overheating, or abnormal liquid levels where the application requires it. Integrated into the machine’s protection circuit, they enable a protective response that helps prevent motor damage and nuisance shutdowns.
Interface relays and time relays also support a stable control core. Interface relays electrically isolate PLC outputs from field loads, protecting sensitive automation equipment from voltage spikes, surges, and electrical noise. Time relays can stagger motor starts to limit inrush current or keep ventilation fans running after shutdown to dissipate heat.
Make safety faults visible
Series-connected mechanical door switches can hide faults when multiple guards are opened and closed. This “fault masking” can limit a circuit’s achievable safety level, and an accumulation of faults can lead to a loss of safety altogether. A general trip indication complicates troubleshooting by identifying a safety-circuit stop without revealing which device triggered it.
Non-contact safety sensors with DYNlink signal monitoring provide an alternative. Suitable sensors and compatible safety controllers can support series connections while achieving the highest level of safety, Category 4 and Performance Level e (PL e), provided the complete safety circuit is designed and validated for those levels. This approach simplifies wiring while preserving high safety performance.
Selecting devices that support individual status reporting also makes stops easier to investigate. With a compatible diagnostic system, maintenance personnel can identify the relevant guard or device—even in a series-connected circuit—rather than tracing the entire circuit to locate the cause of a stop.
Visibility extends to the operator station. Illuminated pushbuttons, indicator lights, and clearly marked emergency stop devices show personnel, with a quick glance, whether a machine is running, stopped, or waiting for a reset. When status is obvious at the panel, operators can restart faster and have less reason to work around a safety stop.
Build a reputation for reliability
Smart factory requirements give OEMs a reason to revisit familiar electrical design choices. The question is not simply whether a component meets its nominal rating, but how it responds to real-world conditions such as supply disturbances, starting demands, and faults.
Treating these choices as part of a coordinated design helps OEMs reduce nuisance stops and simplify troubleshooting. Those benefits extend beyond machine uptime: fewer service issues can help protect warranty margins and build the OEM’s reputation for reliability.
Related reading: 4 technologies that improve system reliability · Designing a machine safety solution for today’s workforce
Authors
Kim Fairley, MBA, Strategic Marketing—OEM · ABB Electrification Business
Kim leads OEM Strategic Marketing at ABB Electrification Business, focusing on driving growth across OEM channels and customer segments in the North American electrification market.
Matt Darroch, Product Marketing Manager · ABB Electrification Business
Matt joined ABB in 2019 as product marketing manager for Pilot Devices, Electronic Relays and Controls, and Limit Switches. He holds a B.S. in Supply Chain Management from East Carolina University.
Jeff Leslie, Product Marketing Specialist · ABB Electrification Business
Jeff is a seasoned Product Marketing Specialist at ABB with nearly 24 years of dedicated experience in machine safety. Throughout his tenure, he has designed safety circuits, bills of materials, electrical drawings, and safety PLC programs, and has supported on‑site installations. In addition to his technical expertise, Jeff plays a key role in training, part setup, advanced technical support, and product management for Safety Products—and, since July, for Softstarters as well. He holds an Electrical Technician diploma from St. Clair College and is certified as a Machinery Safety Expert (CMSE).